
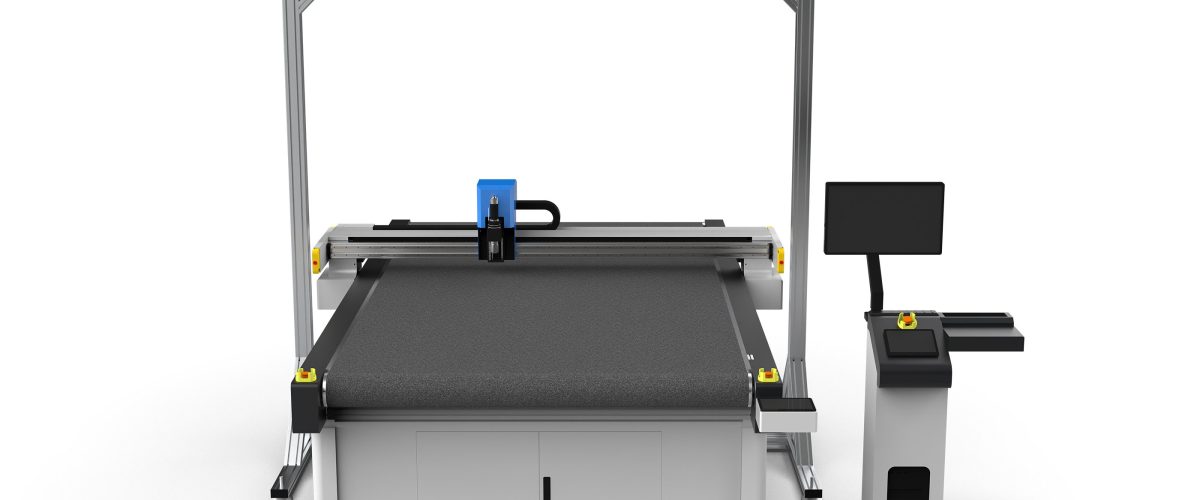
Overview of Fur Cutting Machines
Fur materials (such as wool, rabbit fur, mink, faux fur, etc.) are soft, prone to deformation, prone to static electricity, and tend to shed hair during cutting. Traditional cutting methods have low efficiency and poor precision. The CNC oscillating knife cutting machine performs cold cutting through a high-frequency oscillating blade, requiring no high-temperature laser, thus avoiding burnt edges and material damage, making it an ideal choice for fur cutting. This article provides a practical guide covering equipment selection, process parameters, common problems, and maintenance.
I. Key Selection Parameters for Fur Cutting Machines
1. Cutting working area
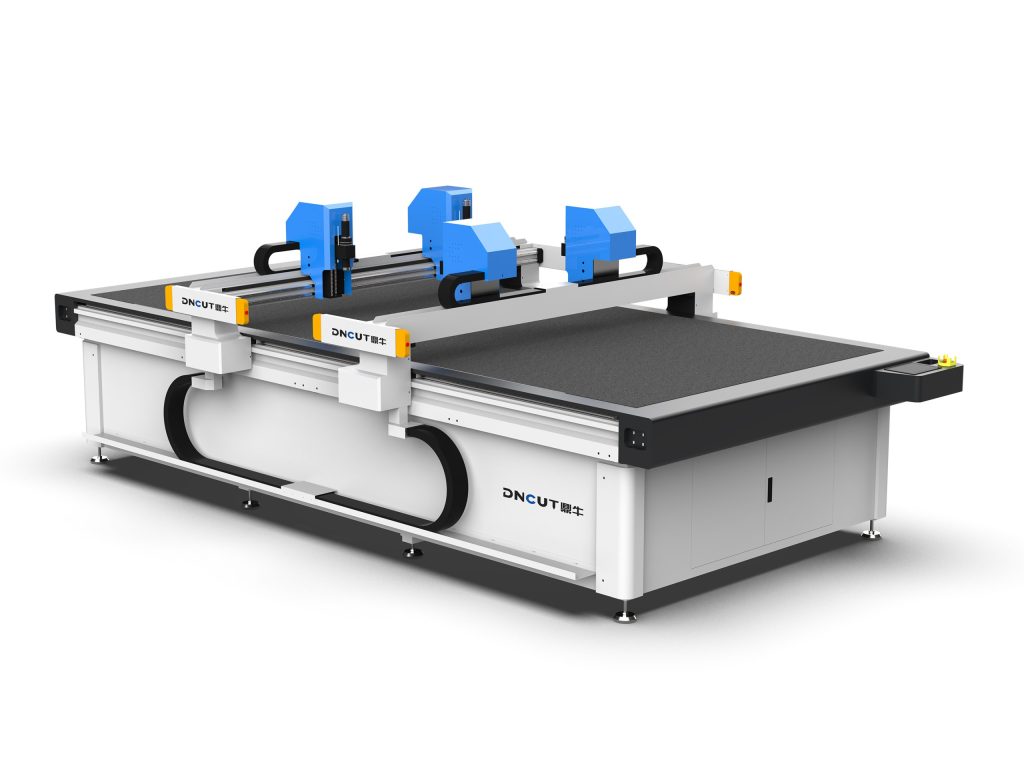
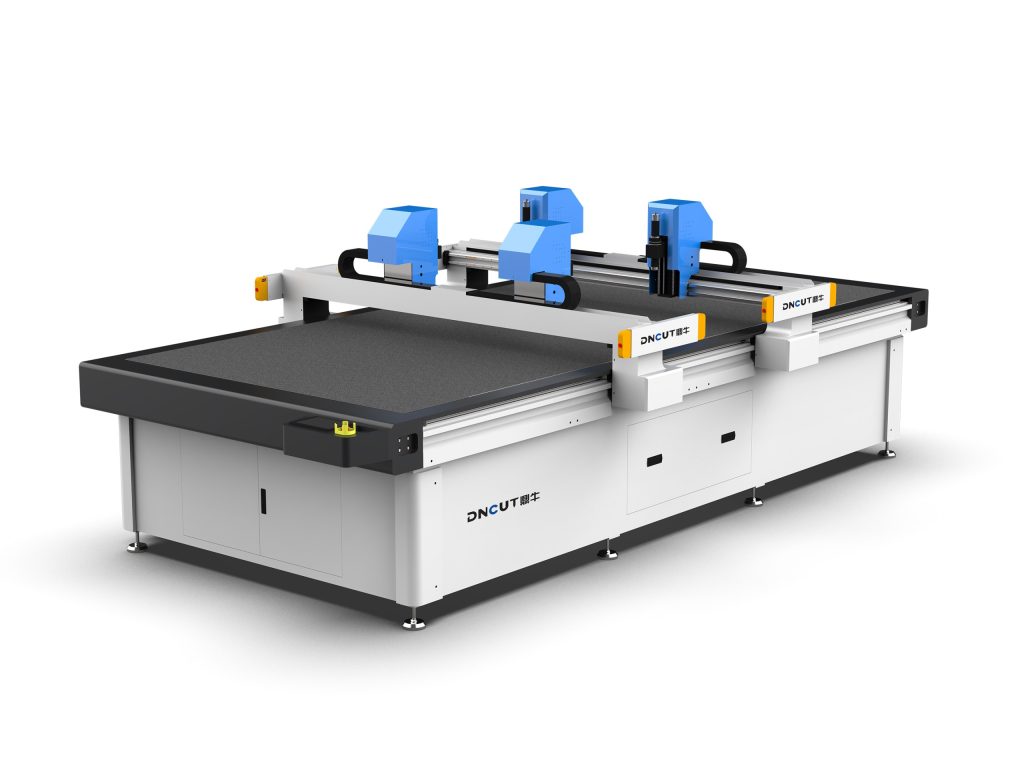
Select based on common fur material sizes and layout requirements. For example, sheepskin materials are typically 60-80cm wide; it is recommended to choose equipment with an effective cutting working area of no less than 1600mm×2500mm, so that multiple pieces of leather can be laid out in one pass. For small-batch, multi-variety production, a small working area model of 1200mm×1200mm can be selected.
2. Oscillating Knife Frequency and Amplitude
The oscillating knife frequency is typically 8000-12000 times per minute, with adjustable amplitude (0.5-5mm). When cutting thick fur (such as plush), the frequency needs to be increased to above 10000 times/min, and the amplitude appropriately increased (2-3mm), to ensure clean cuts and reduce fuzz. When cutting thin fur (such as rabbit fur), the frequency can be reduced to 8000 times/min with an amplitude of 1-2mm, to avoid material displacement caused by excessive vibration.
3. Tool Types
Common tools include:
- Oscillating knife: suitable for most fur and leather, with good cut verticality.
- Round knife: suitable for cutting thicker fur, but the cut is slightly curved.
- drag knife: used for fine pattern cutting, but prone to pulling the fur, requiring vacuum adsorption for fixation.
It is recommended to equip the oscillating knife as standard, with a round knife as a backup option.
4. Vacuum Suction System
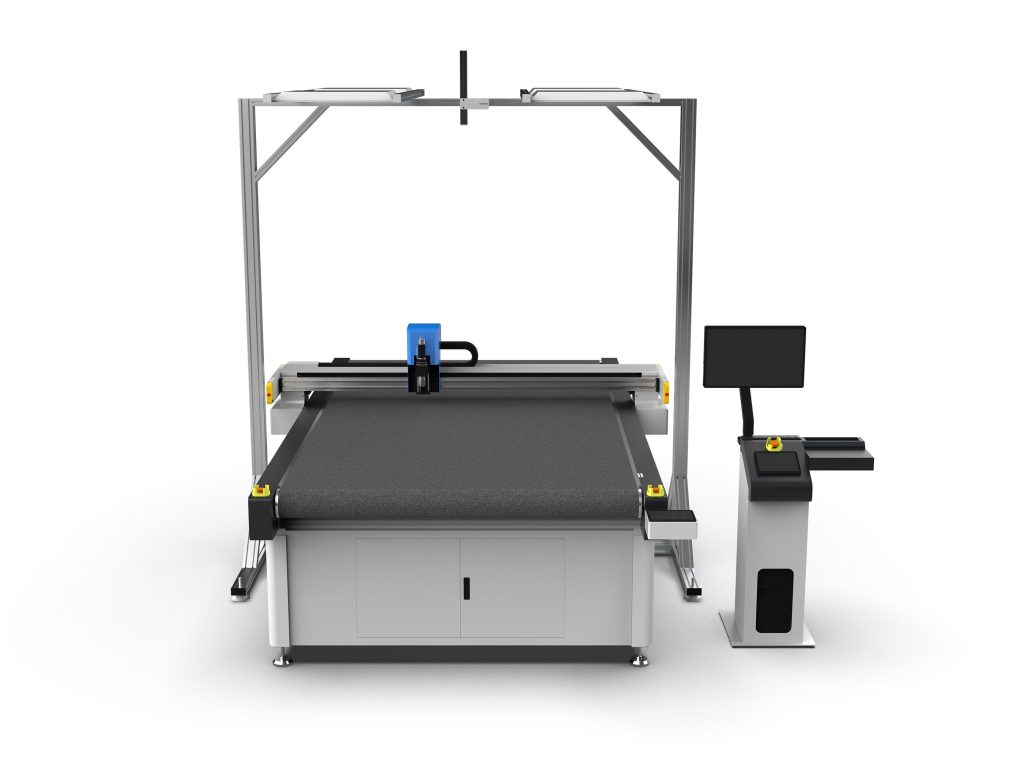
Fur is soft and easy to shift, so a vacuum adsorption system must be equipped. The adsorption force is recommended to be no less than -0.06MPa, and the adsorption area should be controlled by zones to accommodate leather materials of different sizes. For fur with strong air permeability, high-density adsorption pads or covering films are needed to enhance the adsorption effect.
5. Control System and Software
Choose a CNC system that supports common CAD formats (DXF, PLT, AI) and has automatic nesting and path optimization functions. The software should be able to set parameters such as cutting speed, knife pressure, and overcut. Models with a vision positioning system are recommended, as they can automatically identify the leather outline and improve nesting utilization.
II. Setting of Fur Cutting Process Parameters
1. Cutting Speed
Excessive speed can cause rough cuts and material displacement; too slow results in low efficiency and possible scorching (although it is cold cutting, frictional heat can still have an effect). It is recommended to set the initial speed at 300-500mm/s and adjust according to fur thickness and density. For example, mink cutting speed can be set at 400mm/s, and plush at 250mm/s.
2. Knife pressure
Knife pressure determines the force with which the blade is pressed into the material. For thin fur (such as rabbit fur), set the knife pressure to 0.2-0.3MPa; for thick fur (such as sheep shearling), set it to 0.4-0.6MPa. Too much knife pressure can easily cause the underlying material to be cut through or the blade to wear, while too little cannot cut through.
3. Overcut Settings
When cutting closed shapes, an overcut amount must be set (usually 0.5-2mm) to ensure the corners are fully cut through. For fur, the overcut amount should not be too large to avoid damaging adjacent areas.
4. Multi-layer cutting
Fur can be cut in multiple stacked layers, but the layers must be secured to one another. It is recommended to fix each layer with double-sided tape or spray adhesive, with a total thickness not exceeding 20mm. The cutting speed must be reduced accordingly by 20%-30%.
III. Common Problems and Solutions
1. Rough cuts and burrs
Causes: dull blade, too low vibration frequency, too fast speed. Solutions: replace the blade regularly (it is recommended to check every 8 hours), increase the vibration frequency to above 10,000 times/min, and reduce the cutting speed to below 300mm/s.
2. Material displacement
Cause: insufficient suction, excessive knife pressure, or speed too high. Solution: Check the vacuum pump and suction pad sealing, and increase suction; reduce knife pressure and speed; for small pieces, add auxiliary suction fixtures.
3. Incomplete Cutting
Cause: Insufficient blade extension length, too low knife pressure, insufficient overcut. Solution: Adjust the blade extension length (usually 0.5-1mm more than the material thickness), increase the knife pressure, and set the overcut to 1-2mm.
4. Static electricity causes lint adsorption
Fur easily generates static electricity, and lint adheres to the table and guide rails. Solution: Install an ion blower to eliminate static electricity, clean the table regularly, and use anti-static adsorption pads.
IV. Maintenance and Care
1. Daily cleaning
After each shift, use a vacuum cleaner to remove lint from the table, guide rails, and knife head area. Prevent lint from entering the guide rails and lead screws, which can cause wear.
2. Blade replacement
Cutting quality degrades after blade wear, so replace blades promptly. When replacing, pay attention to the blade orientation and calibrate the perpendicularity between the blade and the table. It is recommended to stock commonly used blades.
3. Vacuum system maintenance
Check the vacuum pump oil level weekly (if it is an oil pump), clean off lint from the surface of the vacuum pad, and check whether the piping leaks. Replace damaged vacuum pads promptly.
4. Transmission system lubrication
Clean the guide rails and lead screws monthly and apply lubricating grease. For fur processing environments, dust-resistant lubricating grease is recommended.
V. Summary of selection recommendations
When choosing a fur cutting machine, prioritize the oscillating knife model, determine the working area based on production volume, ensure the vacuum adsorption system is powerful and reliable, and the software must support automatic nesting and vision positioning. Process parameters need to be adjusted according to the type of fur, and the optimal combination should be determined through trial cuts. Daily maintenance focuses on cleaning and blade management. Following the above guidelines can significantly improve cutting quality and production efficiency.