
Corrugated cardboard sample cutting machine: a full-process analysis from model selection to efficient application
The corrugated cardboard sample cutting machine is the core equipment for packaging enterprises to achieve rapid prototyping and small-batch production. Compared with laser cutting or traditional die cutting, the CNC oscillating knife cutting machine has advantages in corrugated cardboard processing such as no smoke or dust, no scorched edges, and low cost. Based on actual production experience, this article systematically sorts out equipment selection, operating key points, and maintenance strategies to help you maximize equipment value.
I. Core types and applicable scenarios of corrugated cardboard sample cutting machines
According to the cutting principle, mainstream equipment is divided into three categories:
- Flatbed sample cutting machine: The worktable is fixed, and the knife moves in the X-Y directions. Suitable for precision proofing of single sheets of corrugated cardboard (thickness 1-10mm), with repeat positioning accuracy up to ±0.1mm. Common table sizes include 1300×2500mm and 1600×3000mm, suitable for carton factories and display stand production.
- Roll-fed sample cutting machine: Equipped with feed rollers, it can continuously process rolled corrugated paper, with efficiency 30%-50% higher than flatbed machines. Suitable for producing die-cut samples of the same pattern in large batches.
- Hybrid type (flatbed + roll-fed): Combines flexibility and efficiency, but at a higher price. Suitable for enterprises with many order types and medium batch sizes.
When selecting a model, pay attention to: maximum cutting thickness (corrugated cardboard is usually ≤15mm), knife type (oscillating knife, circular knife, creasing wheel), control system (whether it supports direct import of DXF/PLT) and the number of vacuum adsorption zones (the more zones, the more stable the fixation of small-sized samples).
II. Key Parameter Settings and Operating Points
2.1 Tool Selection and Parameters
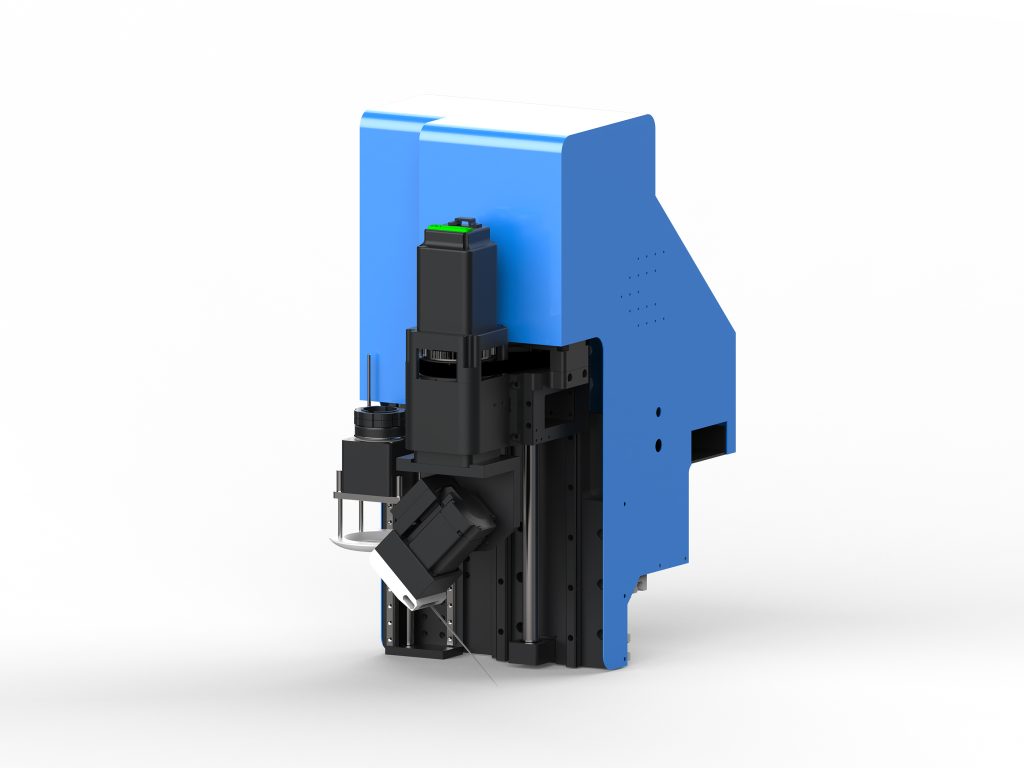
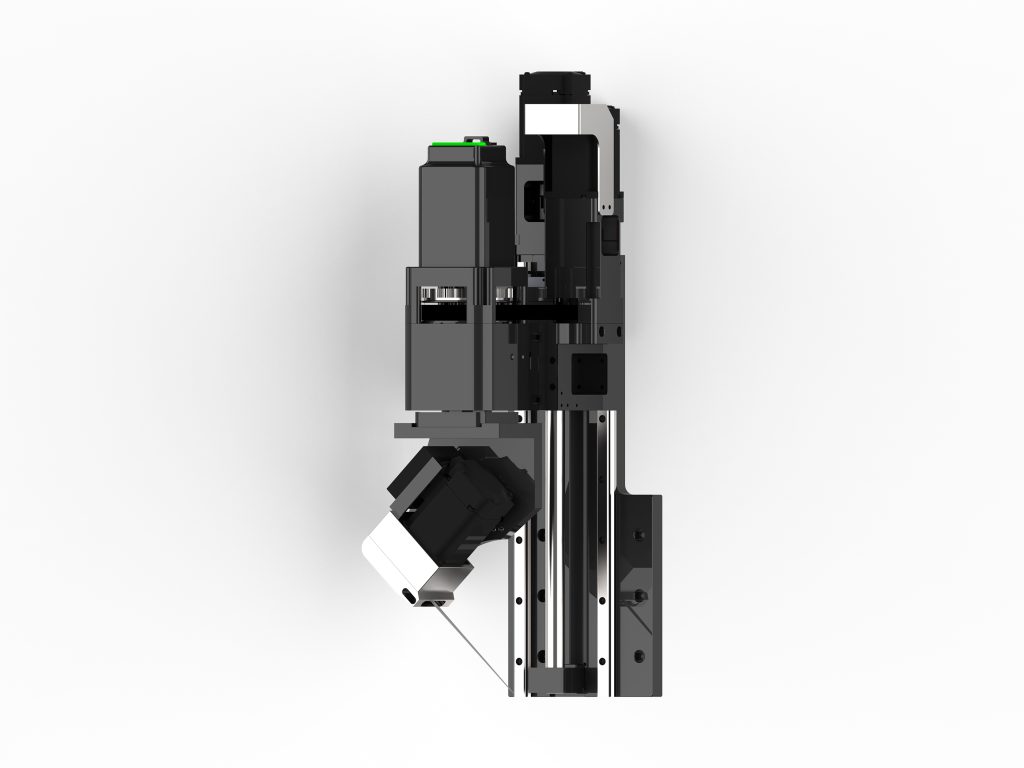
Corrugated cardboard consists of top liner, fluting, and bottom liner, and is prone to burrs or crushing during cutting. It is recommended to use an oscillating knife (frequency 8000-12000 times/min) with a tungsten carbide blade, with a blade angle of 30°-45°. Recommended cutting speeds: 800-1200mm/s for three-layer corrugated cardboard (thickness 3-5mm); 500-800mm/s for five-layer (thickness 6-8mm); 300-500mm/s for seven-layer (thickness 9-12mm). Too fast a speed will cause tearing at the cut, while too slow will cause burning or adhesion.
2.2 Vacuum Adsorption and Fixation
Corrugated cardboard has high air permeability, so it is necessary to ensure the vacuum adsorption force is ≥0.6MPa. For small-sized samples (such as 100×100mm), local adsorption zones should be activated, and masking tape should be used to help seal the edges. If the cardboard is warped, it can be pre-pressed first or fixed with double-sided tape.
2.3 Creasing and Cutting Sequence
The pressure of the creasing wheel needs to be adjusted according to the cardboard thickness: use 0.2-0.3MPa for three-layer cardboard, and 0.4-0.5MPa for five-layer cardboard. The cutting sequence should follow “inside first, then outside; small first, then large” to avoid displacement caused by changes in adsorption force. For samples that need to be folded, the creasing depth should be controlled at 30%-40% of the cardboard thickness.
III. Common Problems and Solutions
3.1 Burrs or delamination at the cut edge
Causes: worn blade, excessive speed, insufficient suction. Countermeasures: inspect the blade every 200-300 meters of cutting and replace it promptly once worn; reduce the speed by 10%-20%; add suction zones or use auxiliary pressure strips.
3.2 Dimensional deviation out of tolerance
Causes: loose belt, worn guide rails, or incorrect file scale. Countermeasures: calibrate the X-Y axis positioning accuracy once a month (test with a standard circle); check whether the file unit is millimeters; tension the timing belt (deflection ≤5mm).
3.3 Unclear crease lines or cracking
Cause: Insufficient pressure or worn creasing wheel. Solution: Gradually increase pressure until a clear groove appears on the cardboard without cracking; replace the creasing wheel (service life approximately 500,000 meters); for high-grammage face paper, preheat to 40-50°C before creasing.
IV. Maintenance and Efficiency Improvement
4.1 Daily Maintenance Checklist
- Each shift: Clean paper scraps from the table surface, check whether the vacuum pipeline is blocked.
- Weekly: Clean the guide rails and apply lithium-based grease, check the blade clamping force.
- Monthly: Calibrate the origin sensor, test the emergency stop function, check the belt tension.
- Quarterly: Replace the vacuum pump filter, check the airtightness of the air circuit.
4.2 Efficiency Improvement Tips
Turn commonly used carton structures (such as 0201, A1, etc.) into parametric templates to reduce drawing time; use nesting software to nest multiple samples to improve material utilization; for repeat orders, save tool paths and parameter presets. Actual case: A carton factory, by optimizing nesting and presetting parameters, reduced proofing time from an average of 45 minutes/piece to 22 minutes/piece.
V. Selection Recommendations and Return on Investment
It is recommended to choose based on the average daily proofing volume: for ≤20 pieces per day, choose an entry-level flatbed model (approximately 80,000-120,000 RMB); for 20-50 pieces, choose a mid-range flatbed model with automatic tool changing (150,000-250,000 RMB); for >50 pieces or when roll material processing is required, choose a hybrid model (over 300,000 RMB). In terms of return on investment, one sample cutting machine can replace 2-3 skilled proofing workers. Calculated at 5,000 pieces of proofing per year, the cost can be recovered in approximately 12-18 months. Pay close attention to the manufacturer’s after-sales response time (recommended ≤24 hours) and software upgrade support.
The value of a corrugated cardboard sample cutting machine lies not only in replacing manual labor, but also in bridging the rapid verification link between design and production. Reasonable selection, careful operation, and regular maintenance can keep the equipment running stably over the long term, creating sustained competitiveness for packaging enterprises.