
Carbon Fiber Cutting Machine: A Complete Guide from Selection to Efficient Production
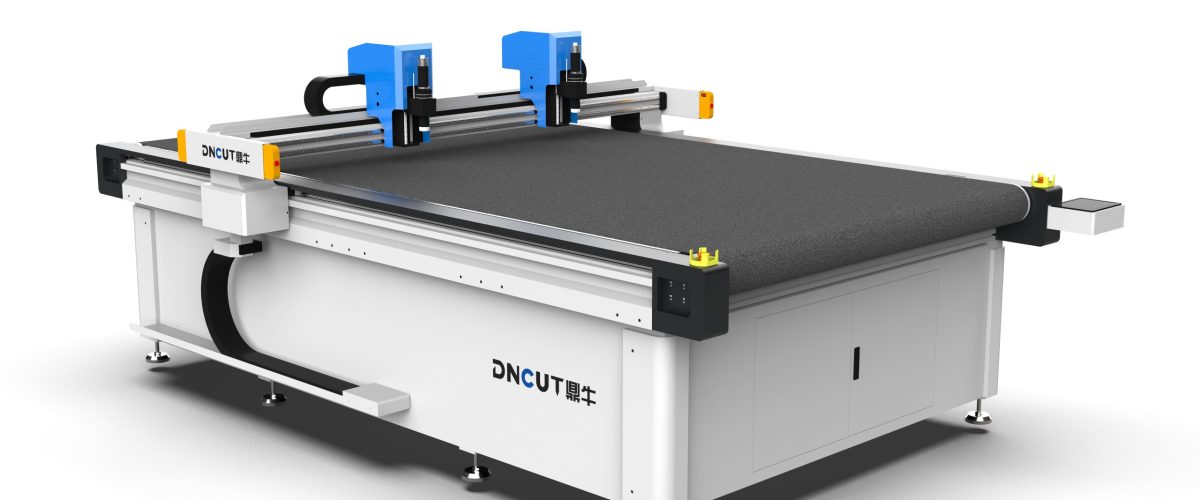
Carbon fiber composite materials are increasingly widely used in aerospace, automotive, sports equipment, and other fields due to their lightweight and high-strength characteristics. However, cutting and processing carbon fiber faces many challenges: heavy dust, rapid tool wear, and high cutting precision requirements. Carbon fiber cutting machines (i.e., CNC oscillating knife cutting machines) have become mainstream processing equipment for carbon fiber prepreg, cured sheets, fabrics, and other materials thanks to their cold cutting, no heat-affected zone, and high precision. This article focuses on the selection parameters, operating points, and maintenance strategies for carbon fiber cutting machines, providing practical references that can be implemented.
I. Analysis of Core Technical Parameters of Carbon Fiber Cutting Machines
When purchasing a carbon fiber cutting machine, the following parameters directly determine cutting capability and production efficiency and should be comprehensively evaluated based on one’s own material characteristics and capacity requirements.
1. Cutting Head Type and Amplitude
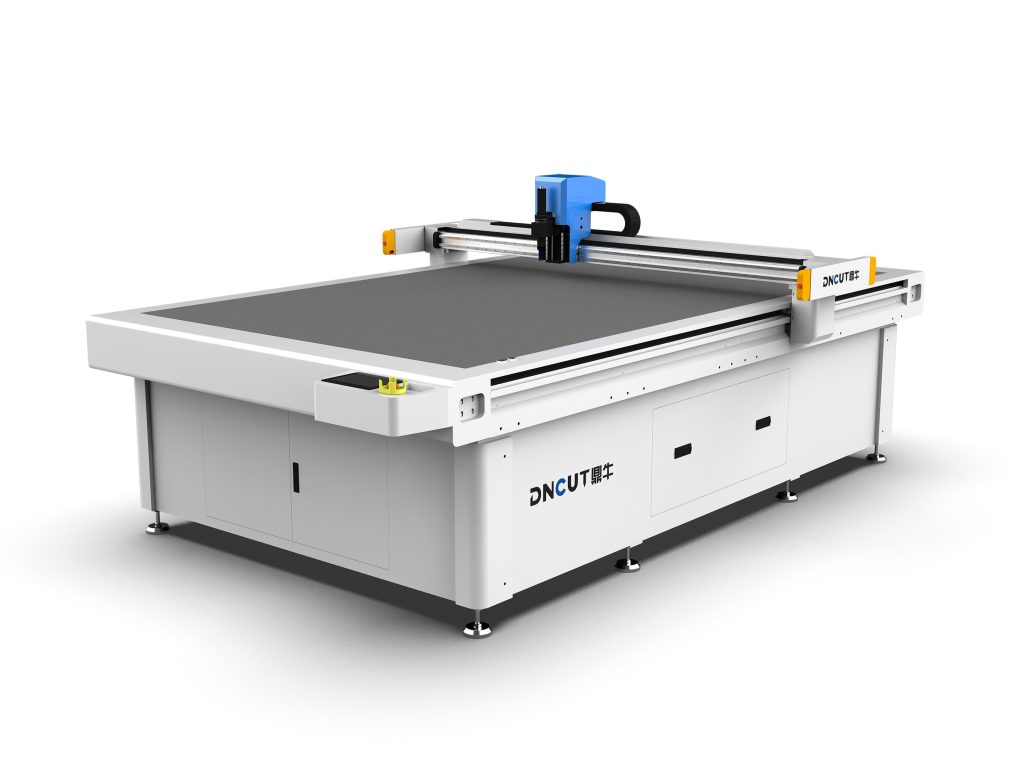
Carbon fiber cutting machines are usually equipped with an oscillating knife (also called a vibrating knife) or a drag knife. For prepreg or fabric with a thickness of ≤5 mm, a high-frequency low-amplitude oscillating knife (amplitude 0.5-1.5 mm, frequency 8000-12000 times/min) can reduce material delamination and burrs; for cured sheets with a thickness of 5-15 mm, a large-amplitude (2-3 mm) or pneumatic knife should be selected. Some high-end models support quick-change cutting heads to accommodate different processes.
2. Positioning Accuracy and Repeat Positioning Accuracy
Carbon fiber parts often have strict contour tolerances, so it is recommended to choose equipment with positioning accuracy ≤±0.1 mm and repeat positioning accuracy ≤±0.05 mm. A structure using servo motors + precision reducers + linear guides can ensure long-term stability. For scenarios requiring multi-layer cutting (such as prepreg layup), repeat positioning accuracy is particularly critical; otherwise, interlayer misalignment will cause parts to be scrapped.
3. Working Table and Vacuum Adsorption System
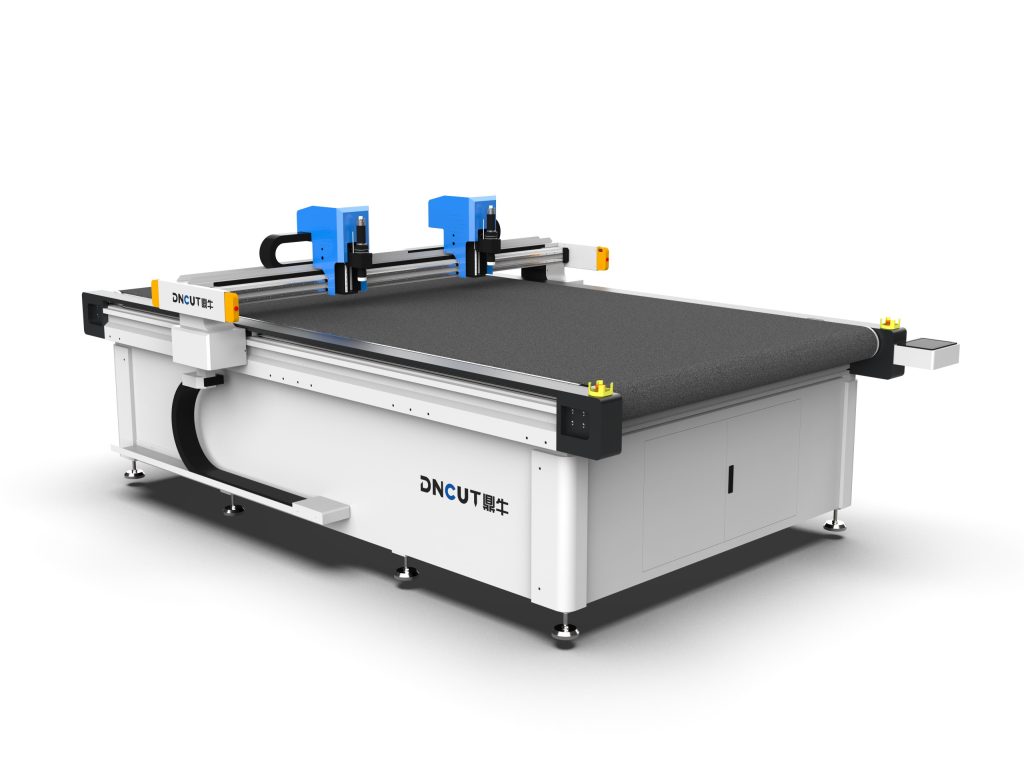
The table size needs to be determined according to the maximum workpiece size, with common specifications being 1600 mm × 2500 mm and 2000 mm × 3000 mm. Carbon fiber cutting generates a large amount of dust, so a zoned vacuum adsorption system must be equipped, with adsorption force ≥20 kPa, to ensure the material does not shift during cutting. The table felt needs to be replaced regularly to prevent dust from embedding and affecting adsorption performance.
4. Cutting Speed and Acceleration
Cutting speed is affected by material thickness, tool type, and pattern complexity. For 1 mm thick carbon fiber prepreg, the oscillating knife cutting speed can reach 30-50 m/min; for 5 mm thick cured sheets, the speed drops to 5-10 m/min. Acceleration is recommended to be ≥1g to reduce idle travel time and improve overall efficiency. However, note that excessive acceleration may cause table vibration and affect cutting quality.
5. Dust Removal System
Carbon fiber dust is conductive and prone to floating, so a high-efficiency dust removal device must be equipped. It is recommended to choose models with a follow-up dust hood, with the suction inlet as close as possible to the cutting point, air volume ≥2000 m³/h, and filtration accuracy ≤5 μm. Poor dust removal not only harms health but also causes dust to accumulate on guide rails and racks, accelerating equipment wear.
II. Operating Techniques and Process Optimization for Carbon Fiber Cutting Machines
Correct operating methods and process parameter settings can significantly improve cutting quality and tool life.
1. Tool Selection and Replacement Cycle
For cutting carbon fiber prepreg, carbide oscillating knives with a blade angle of 30°-45° are recommended for higher sharpness; for cutting cured sheets, diamond-coated tools are selected, improving wear resistance by 3-5 times. After tool wear, cutting force increases, leading to material edge burrs and delamination. It is recommended to check the blade edge every 200-300 meters of cutting (prepreg) or 50-80 meters (cured sheets) and replace it in time. Wear degree can be judged by listening to the cutting sound or observing chip morphology.
2. Cutting Parameter Matching
Taking 1 mm thick carbon fiber prepreg as an example: oscillation frequency 10000 times/min, amplitude 1 mm, feed speed 40 m/min, vacuum adsorption pressure 25 kPa. For 3 mm thick cured sheets: frequency 8000 times/min, amplitude 2 mm, feed speed 8 m/min; layered cutting is recommended (1-1.5 mm per layer) to avoid edge cracking caused by cutting through in a single pass. Actual parameters need to be fine-tuned according to material resin content and fiber orientation; trial cutting is recommended first.
3. Layout and Path Optimization
Use CAD/CAM software for intelligent nesting to improve material utilization. For carbon fiber fabrics, pay attention to the influence of warp and weft directions on cutting quality, and try to make the cutting path form a certain angle with the fiber direction (such as 15°-30°) to reduce fiber tearing. Using common-edge cutting and bridge connections can reduce idle travel and improve efficiency. For small holes and sharp corners, the feed speed can be reduced to 50%-70% of the normal value, and arc transitions can be used.
4. Interlayer Control in Multi-layer Cutting
When cutting multi-layer prepreg, layers tend to slide. In addition to increasing vacuum adsorption force, the following measures can be taken: spray a small amount of water or special adhesive between layers; use a spiked pressure plate; reduce cutting speed to decrease lateral force. Generally, it is recommended that a single stack not exceed 10 layers (prepreg), and each layer should have consistent thickness.
III. Key Maintenance and Care Points for Carbon Fiber Cutting Machines
Carbon fiber dust is conductive and abrasive, so regular maintenance is key to ensuring equipment life and precision.
1. Daily Cleaning
After each shift, use a vacuum cleaner to remove dust from the table, guide rails, racks, and tool head area. Do not use compressed air to blow off dust, to prevent dust from entering the electrical cabinet. Check whether the vacuum pipeline is blocked and clean the dust collection box.
2. Weekly Inspection
Check the air gap of the tool head oscillation mechanism (usually 0.05-0.1 mm); if too large, it may cause unstable amplitude. Check the tension of the timing belt; if too loose, it will cause positioning deviation. Clean the linear guides and apply special lubricating grease (such as lithium-based grease), but avoid excessive grease that attracts dust.
3. Monthly Maintenance
Check the vacuum pump filter and clean or replace the filter element; check the electrical cabinet cooling fan and remove accumulated dust; calibrate the equipment origin and parallelism, and use a dial indicator to detect table flatness (error ≤0.1 mm/m). For high-precision processing, it is recommended to perform a laser interferometer accuracy test quarterly.
4. Tool Management
Establish tool life records and record the cutting length and material type of each tool. Worn tools can be downgraded for rough cutting or non-critical parts. Use special tool boxes when storing tools to avoid blade edge collisions.
IV. Common Problems and Solutions
- Burrs or delamination at cutting edges: Check whether the tool is worn, reduce feed speed, increase oscillation frequency, and ensure sufficient vacuum adsorption force.
- Decreased cutting precision: Check guide rail lubrication and timing belt tension, calibrate the origin, and clean dust accumulation on the racks.
- Serious dust flying: Check whether the dust hood is positioned at the cutting point, whether the suction air volume is sufficient, and whether the pipeline is leaking.
- Abnormal noise from the tool head: Check whether the bearings of the oscillation mechanism are damaged, whether the air gap is too large, or whether the fastening screws are loose.
V. Selection Recommendations and Summary
The selection of a carbon fiber cutting machine should be based on material type, thickness range, precision requirements, and capacity planning. For users mainly cutting prepreg, priority should be given to high-frequency oscillating knives and dust removal systems; for cured sheet processing, emphasis should be placed on a rigid table and large-amplitude tool heads. It is recommended to provide material samples for trial cutting before purchase to verify the actual cutting effect of the equipment. In daily use, strictly implementing cleaning and maintenance plans can extend equipment life by more than 30%. Through reasonable tool management and process parameter optimization, carbon fiber cutting machines can stably achieve high-quality, high-efficiency cutting production.