
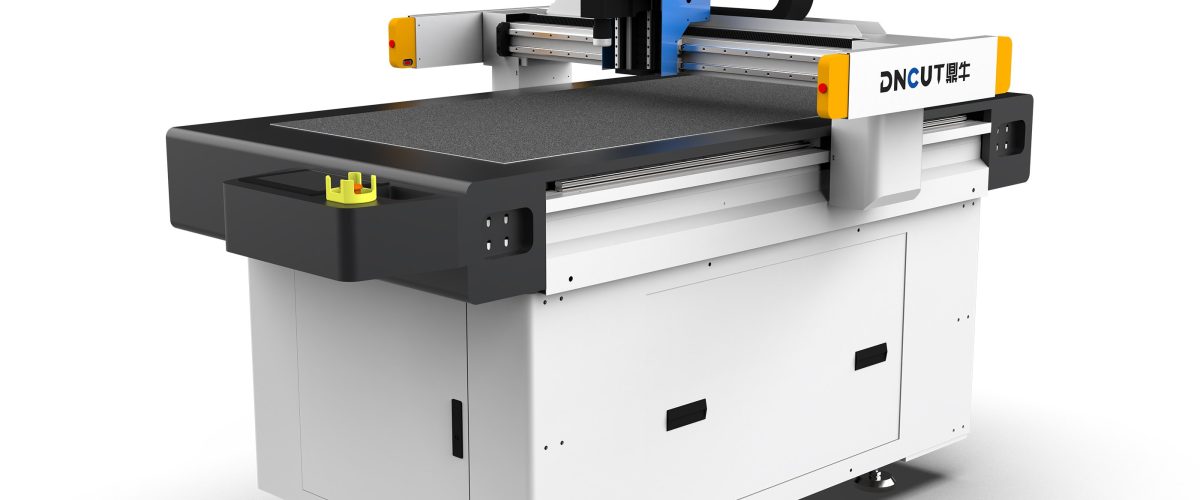
탄소섬유 재단기: 선정부터 고효율 생산까지의 완벽 가이드
Carbon fiber composites are increasingly applied in aerospace, automotive, and sports equipment industries due to their lightweight and high-strength characteristics. However, cutting carbon fiber involves numerous challenges, including excessive dust generation, rapid tool wear, and high precision requirements. Oscillating knife cutting machines (i.e., CNC oscillating knife cutting machines) have become the mainstream equipment for processing materials such as carbon fiber pre-pregs, cured plates, and fabrics, thanks to their cold cutting capability, absence of thermal impact, and high precision. This document provides practical reference guidelines focusing on selection parameters, operational tips, and maintenance strategies for carbon fiber cutting machines.
1. 탄소섬유 재단기의 핵심 기술 파라미터 분석
탄소섬유 재단기를 구매할 때 다음 파라미터는 절단 능력과 생산 효율을 직접 결정하므로, 자체 재료 특성과 생산 능력 요구를 종합적으로 평가해야 합니다.
1. 절단 헤드 유형 및 진폭
Carbon fiber cutting machines typically come equipped with an oscillating knife (also known as a vibration knife) or a drag knife. For prepreg or fabric materials with thickness ≤5mm, a high-frequency, low-amplitude oscillating knife (amplitude 0.5-1.5mm, frequency 8000-12000 times/min) can reduce material delamination and burrs. For cured plates with thickness between 5-15mm, a large-amplitude (2-3mm) or pneumatic knife should be selected. Some advanced models support quick-change heads to adapt to various processes.
2. 위치 결정 정밀도 및 반복 정밀도
탄소섬유 부품은 종종 엄격한 윤곽 공차를 가지므로, 위치 결정 정밀도 ≤±0.1mm, 반복 정밀도 ≤±0.05mm의 장비를 선택하는 것이 좋습니다. 서보 모터 + 정밀 감속기 + 리니어 가이드 구조를 채택하면 장기적인 안정성을 보장할 수 있습니다. 다층 절단(예: 프리프레그 적층)이 필요한 시나리오에서는 반복 정밀도가 특히 중요하며, 그렇지 않으면 층간 어긋남으로 인해 부품이 폐기될 수 있습니다.
3. 작업 테이블 및 흡착 시스템
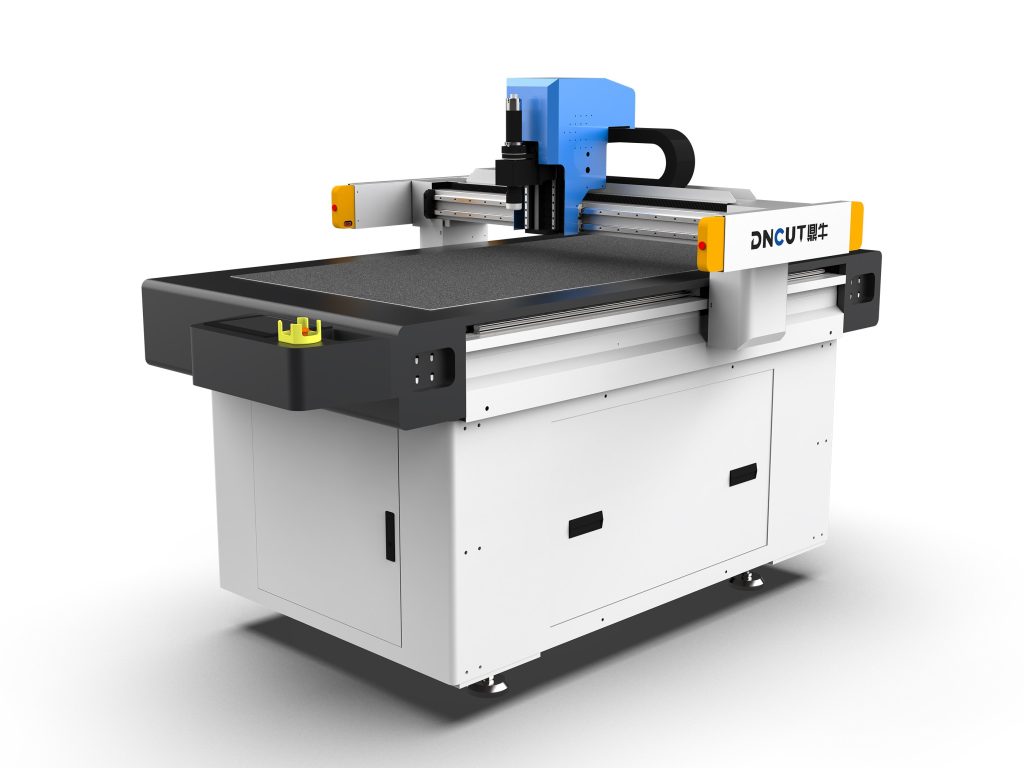
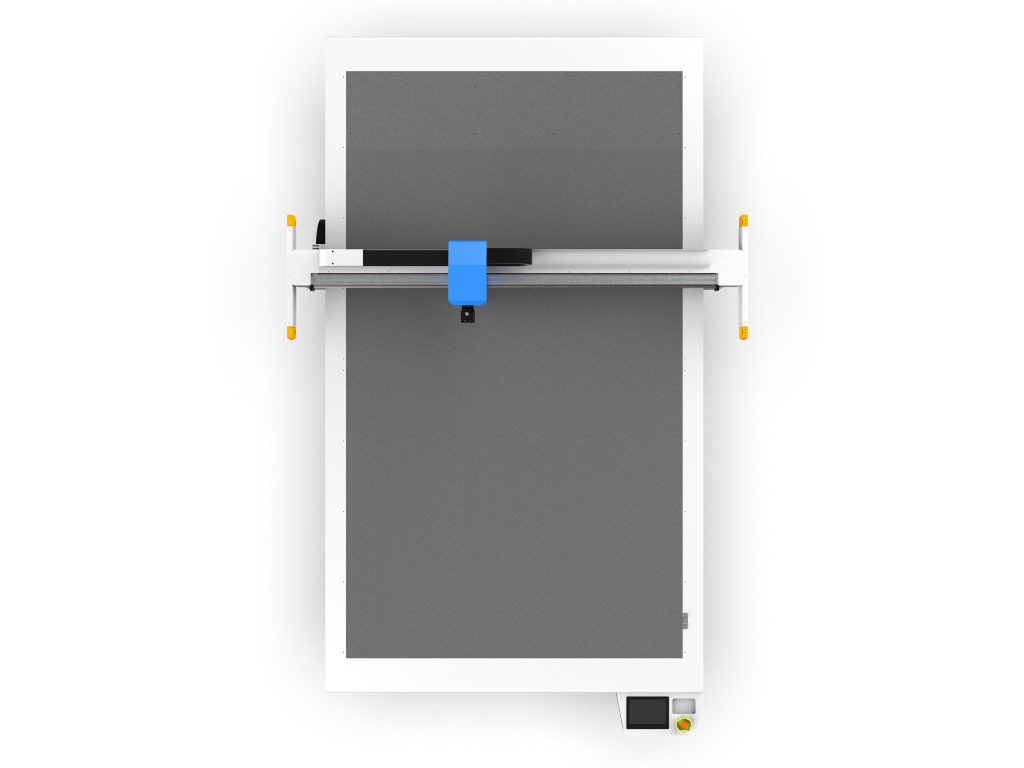
The table size must be determined according to the maximum workpiece size, with common specifications being 1600mm×2500mm and 2000mm×3000mm. Carbon fiber cutting generates a large amount of dust, so a zone-specific vacuum suction system must be installed, with suction force ≥20kPa to ensure the material does not shift during cutting. The table felt should be replaced regularly to prevent dust accumulation from affecting suction performance.
4. 절단 속도 및 가속도
절단 속도는 재료 두께, 공구 유형 및 패턴 복잡성의 영향을 받습니다. 1mm 두께 탄소섬유 프리프레그의 경우, 진동칼 절단 속도는 30-50m/min에 달할 수 있습니다. 5mm 두께 경화판의 경우, 속도는 5-10m/min으로 감소합니다. 가속도는 ≥1g를 권장하여 공회전 시간을 줄이고 전체 효율을 향상시킵니다. 그러나 과도한 가속도는 테이블 진동을 유발하여 절단 품질에 영향을 미칠 수 있으므로 주의해야 합니다.
5. 집진 시스템
탄소섬유 분진은 전도성이 있으며 공기 중에 쉽게 부유하므로 고효율 집진 장치를 반드시 갖추어야 합니다. 흡입 후드가 있는 모델을 선택하고, 흡입구를 절단 위치에 가능한 한 가까이 배치하며, 공기량 ≥2000m³/h, 여과 정밀도 ≤5μm를 권장합니다. 집진 효과가 불충분할 경우 건강에 해롭게 작용할 뿐만 아니라, 분진이 가이드 레일 및 랙에 쌓여 장비의 마모를 가속화합니다.
2. 탄소섬유 재단기의 조작 기술 및 공정 최적화
올바른 조작 방법과 공정 파라미터 설정은 절단 품질과 공구 수명을 현저히 향상시킬 수 있습니다.
1. 공구 선택 및 교체 주기
탄소섬유 프리프레그 절단에는 초경합금 진동칼을 권장하며, 날 각도 30°-45°로 예리도가 더 높습니다. 경화판 절단에는 다이아몬드 코팅 공구를 선택하며, 내마모성이 3-5배 향상됩니다. 공구가 마모되면 절단력이 증가하여 재료 가장자리에 버와 분층이 발생하므로, 200-300m(프리프레그) 또는 50-80m(경화판) 절단마다 날을 점검하고 적시에 교체하는 것이 좋습니다. 절단 소리를 듣거나 칩 형태를 관찰하여 마모 정도를 판단할 수 있습니다.
2. 절단 파라미터 매칭
1mm 두께 탄소섬유 프리프레그를 예로 들면: 진동 주파수 10000회/분, 진폭 1mm, 이송 속도 40m/min, 진공 흡착 압력 25kPa. 3mm 두께 경화판의 경우: 주파수 8000회/분, 진폭 2mm, 이송 속도 8m/min, 분층 절단(층당 1-1.5mm)을 권장하여 한 번에 절단하여 가장자리가 깨지는 것을 방지합니다. 실제 파라미터는 재료 수지 함량, 섬유 방향에 따라 미세 조정해야 하며, 먼저 시험 절단하는 것이 좋습니다.
3. 레이아웃 및 경로 최적화
Improves material utilization through intelligent layout using CAD/CAM software. For carbon fiber fabric, pay attention to the impact of warp and weft directions on cutting quality, and ensure the cutting path forms a specific angle (e.g., 15°-30°) with the fiber direction to reduce fiber pulling. Using shared edge cutting and bridge connections can reduce idle running and improve efficiency. For small holes and sharp corners, reduce feed speed to 50%-70% of normal value and use arc transitions.
4. 다층 절단의 층간 제어
When cutting multi-layer pre-preg, delamination between layers is prone to occur. In addition to increasing vacuum suction force, the following measures can be taken: spraying a small amount of water or specialized adhesive between layers; using a pressure plate with spikes; reducing cutting speed to minimize lateral forces. It is generally recommended not to exceed 10 layers (pre-preg) for single-layer cutting, and each layer thickness should be consistent.
3. 탄소섬유 재단기의 유지보수 및 관리 요점
탄소섬유 분진은 전도성과 연마성이 있으므로, 정기적인 유지보수는 장비 수명과 정밀도를 보장하는 핵심입니다.
1. 일일 청소
Clean dust from the table, guide rails, rack, and tool head area with a vacuum cleaner after each shift change. Do not blow with compressed air, as dust may enter the electrical cabinet. Check for clogged dust extraction pipes and clean the dust collector.
2. 주간 점검
공구 헤드 진동 기구의 에어 갭(일반적으로 0.05-0.1mm)을 점검합니다. 너무 크면 진폭이 불안정해질 수 있습니다. 동기 벨트 장력을 점검합니다. 너무 느슨하면 위치 편차가 발생할 수 있습니다. 리니어 가이드를 청소하고 전용 윤활 그리스(예: 리튬 기반 그리스)를 도포하지만, 과도한 분진 흡착을 피해야 합니다.
3. 월간 유지보수
Check the vacuum pump filter and clean or replace the filter element. Inspect the electrical cabinet cooling fan and remove dust. Calibrate the equipment’s reference point and parallelism, and use a dial gauge to check the table flatness (error ≤0.1mm/m). For high-precision machining, it is recommended to perform laser interferometer precision inspection every quarter.
4. 공구 관리
공구 수명 기록을 작성하여 각 공구의 절단 길이와 재료 유형을 기록합니다. 마모된 공구는 거친 절단 또는 비핵심 부위에 하향 사용할 수 있습니다. 공구 보관 시 전용 공구 케이스를 사용하여 날 충돌을 방지합니다.
4. 일반적인 문제 및 해결 방안
- 절단 가장자리 버 또는 분층: 공구 마모 여부를 확인하고, 이송 속도를 낮추고, 진동 주파수를 높이고, 진공 흡착력이 충분한지 확인합니다.
- 절단 정밀도 저하: 가이드 레일 윤활 및 동기 벨트 장력을 점검하고, 원점을 교정하고, 랙의 분진 축적을 청소합니다.
- 분진 비산 심함: Check whether the dust hood is positioned toward the cutting point, if the dust extraction airflow is sufficient, and if there are no pipe leaks.
- 공구 헤드 이상 소음: 진동 기구 베어링 손상 여부, 에어 갭 과대 여부, 또는 고정 나사 풀림 여부를 점검합니다.
5. 선정 제안 및 요약
탄소섬유 재단기의 선정은 재료 유형, 두께 범위, 정밀도 요구 및 생산 능력 계획을 중심으로 이루어져야 합니다. 프리프레그 절단 위주의 사용자는 고주파 진동칼과 집진 시스템을 우선적으로 고려하고, 경화판 가공의 경우 강성 테이블과 대진폭 공구 헤드에 중점을 두어야 합니다. 구매 전 재료 샘플을 제공하여 시험 절단을 통해 장비의 실제 절단 효과를 검증하는 것이 좋습니다. 일상 사용에서 청소 및 유지보수 계획을 엄격히 준수하면 장비 수명을 30% 이상 연장할 수 있습니다. 합리적인 공구 관리와 공정 파라미터 최적화를 통해 탄소섬유 재단기는 안정적으로 고품질, 고효율의 절단 생산을 실현할 수 있습니다.